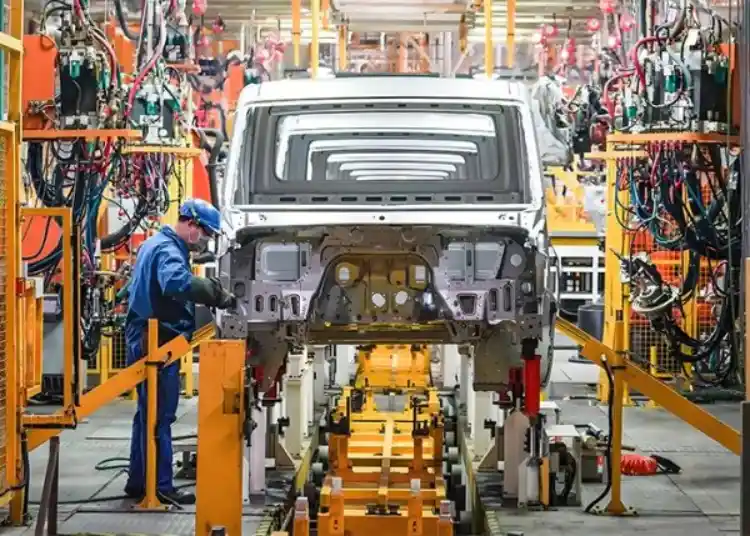
Fixture datums determine where each stamped panel sits before welding, so they have a direct effect on door openings, windshield interfaces, panel gaps, and the repeatability of a cab body in white. A sound fixture does not merely hold sheet metal in place. It creates a stable reference system, controls the joining sequence, and gives dimensional inspection a meaningful baseline.
What a Fixture Datum Controls in a Cab Body in White
A fixture datum is a defined locating reference used to position a panel, subassembly, or body section. In cab welding, the datum network turns several flexible stamped parts into one controlled structure. The important question is not whether the panel touches a locator; it is whether the locators reproduce the design coordinate system from one unit to the next.
From Panel Position to Assembly Interface
A side panel can look correct on its own and still create trouble at final assembly. A few millimetres of movement at the hinge pillar may change the door aperture, while a small shift at the roof rail can affect the windshield flange and seal compression. That is why a body-in-white inspection should connect fixture references to functional interfaces rather than record isolated measurements only.
Three Datum Functions
A practical locating scheme separates three jobs: primary support controls the main plane, secondary locations control movement across that plane, and tertiary locations constrain the remaining degree of freedom. This arrangement prevents over-constraint, which can force a panel into position and release stored stress when clamps open.
How Welding Sequence Protects Dimensional Accuracy
Welding changes the local temperature and creates contraction as the joint cools. The fixture can limit movement, but it cannot cancel an unbalanced sequence. Dimensional quality comes from matching locator stiffness, clamp position, weld order, and heat input to the structure being joined.
Tack Welds Establish the Skeleton
Tack welds should first stabilise the key reference points and interface zones. If long seams are completed before the door aperture, windshield opening, and mounting points are checked, later correction becomes expensive. A better release point is the stable tack-welded skeleton: verify the critical openings, then continue with the planned joining sequence.
Heat Balance Matters More Than Weld Count
More welds do not automatically mean a straighter cab. Concentrating heat on one side of a roof rail or pillar can pull the structure toward the cooling joint. Alternating sides, shortening uninterrupted weld runs, and allowing the fixture to support the panel near the joint reduce the chance of progressive distortion. The exact sequence must be validated against the part geometry and welding process.
A Practical Inspection Plan for Cab Welding Quality
Inspection should follow the same references used in welding. When a measurement is detached from the fixture datum, it is difficult to tell whether the fault began with a stamped panel, a locator, a clamp, or thermal distortion. The following checks create a traceable handover from body-in-white to cab assembly.
| Inspection stage | Qué comprobar | Why it matters | Release decision |
| Before welding | Panel seating, locator contact, clamp reach | Finds gaps or forced fit before heat is added | Reset or correct the locating condition |
| After tack welding | Door and glass openings, mounting points | Confirms the structural skeleton has not moved | Continue only when critical interfaces are stable |
| After full welding | Datum-to-feature dimensions and visible distortion | Separates thermal movement from stamping variation | Repair, rework, or accept against the drawing |
| Before coating | Seams, spatter, drainage and seal areas | Prevents surface preparation from hiding defects | Release only after cleaning and protection checks |
Use Functional Features as Checkpoints
The most valuable checkpoints are the features that another part must meet: hinge locations, latch reinforcement, windshield flange, seat or dashboard mounts, and chassis attachment points. A body can meet a general outer contour measurement and still fail at one of these interfaces. Marking the measurement method, gauge, datum, and inspection timing makes the result repeatable.
Do Not Hide a Fixture Problem with Manual Force
A common shop-floor mistake is to clamp a panel until the gap disappears. That may produce a visually acceptable weld while storing stress in the panel. When the assembly is removed, the gap returns or appears in a neighbouring joint. Check locator wear, clamp alignment, and panel seating first; manual force should not substitute for a corrected reference condition.
Where a Fixture Based Approach Has Limits
Fixtures improve repeatability, but they do not repair poor incoming panels or compensate for an unsuitable joining process. A locating strategy also has a service life. Wear at a pin, pad, or clamp can gradually move the coordinate system without creating an obvious failure on the line.
Two field details deserve attention. First, a locator that is clean at the start of a shift may collect weld spatter later, lifting a panel by a small but consequential amount. Second, a panel can be dimensionally correct while its flange angle is wrong, causing seal compression or adjacent-part fit problems. Cleaning records and flange-angle checks belong in the control plan.
For a project that needs integrated body components and downstream assembly, Shandong TaiRui combines body-component production with stamping, automated welding, lamp assembly, mould processing, and testing resources. Its Capacidades de fabricación are relevant when the same quality logic must carry from formed panels into a repeatable welded structure.
Before approving a finished cab structure, confirm the datum scheme, critical interface tolerances, weld sequence, surface preparation, and inspection records with the manufacturer. ShanDong TaiRui quality assurance includes IATF 16949, ISO 45001, and ISO 14001 certifications within its documented quality and management framework.
The same dimensional logic applies beyond the welding cell: a recent guide on cab body in white manufacturing connects panel forming, fixture location, welding, and inspection into one quality chain.
Three Questions to Settle Before Supplier Approval
Which Features Are the True Body in White Datums?
Ask for the coordinate references used to locate the floor, pillars, roof, openings, and attachment points. If the answer only lists outer panel dimensions, the control plan is incomplete.
How Is Fixture Drift Detected?
Look for a defined check of locator pins, pads, clamps, and gauges, with a reaction plan for wear or spatter. The check should identify when the fixture last matched the approved reference condition.
What Evidence Is Delivered with the Sample?
Request dimensional results tied to the drawing datums, weld inspection records, photographs of critical interfaces, and any approved deviations. A sample without traceable evidence is difficult to scale into stable production.
Preguntas frecuentes
Why Do Fixture Datums Matter in Cab Body in White Welding?
They establish a repeatable coordinate system for panels and subassemblies. That system helps control functional openings, mounting points, panel gaps, and the interfaces used during cab assembly.
Can a Good Fixture Prevent All Welding Distortion?
No. It limits movement, but heat input, weld order, joint design, panel fit, and cooling still influence the result. A stable fixture must work with a validated welding sequence.
What Should Be Checked Before a Cab Body in White Is Released?
Check critical datum-to-feature dimensions, door and windshield openings, attachment points, weld spatter, seam condition, drainage paths, and surface preparation. Record the measurement method and reaction for any out-of-tolerance result.